Conveyor belt separators are an integral component of conveyor system efficiency, playing a critical role in maintaining the cleanliness of conveyor belts and ensuring the smooth operation of the entire system. These tools are designed to remove residual material from the belt, which is crucial for the longevity and efficiency of the conveyor system. Understanding the importance, types, and maintenance of belt scrapers can significantly enhance conveyor operations in any industry reliant on bulk material handling.
What is a Belt Scraper?
Conveyor Belt Cleaning and Metal Detection
A belt scraper is a device installed at various points along a metal detector in conveyor belt and is used to remove material sticking to the conveyor belt. There are primarily two types of belt scrapers: primary scrapers, which remove the bulk of the material, and secondary scrapers, which remove finer particles that the primary scraper may have missed. This differentiation helps industries select the appropriate scraper type based on their specific material handling requirements, ensuring thorough cleaning and minimal carryback.
Importance of Belt Scrapers in Conveyor Operations
The primary importance of a Conveyor metal detector lies in their ability to maintain the efficiency of the conveyor belt by preventing material build-up. This build-up can lead to belt misalignment, which is a common cause of significant wear and tear on the conveyor system. Additionally, clean belts reduce the risk of slip and fall accidents around the conveyor system, thereby enhancing operational safety. These factors make belt scrapers a crucial investment for any operation where bulk material handling is a routine.
Key Benefits of Implementing Belt Scrapers
Implementing belt scrapers in a conveyor system leads to multiple operational benefits. Firstly, they enhance the performance of the belt by ensuring that it is free from residual materials, which can contribute to belt slippage or misalignment. Secondly, they reduce the overall maintenance cost of the conveyor system by minimising wear and tear on both the belt and the rollers. This, in turn, leads to increased longevity of the conveyor parts and reduces the frequency of repairs and replacements.
Design Features of Effective Belt Scrapers
The design of effective belt scrapers is focused on durability and efficiency. Materials like polyurethane or hardened steel are commonly used for the scraper blades, providing a balance between hardness (to scrape effectively) and flexibility (to avoid damaging the belt). Additionally, the design includes features such as easy adjustability to maintain optimal pressure against the belt and quick-change mechanisms to facilitate easy replacement of worn blades. These features ensure that the scraper performs its function efficiently over an extended period.
Installation Guidelines for Belt Scrapers
Proper magnet installation is crucial for the optimal performance of belt scrapers. This process involves aligning the scraper accurately against the conveyor belt to ensure effective cleaning without causing damage to the belt. The installation should also consider the environmental conditions and the type of material being handled, as these factors influence the wear and performance of the scraper blades. Detailed manufacturer guidelines and professional installation services can ensure that the belt scrapers are set up to deliver maximum performance and longevity.
Maintaining Your Belt Scrapers
Maintenance of belt scrapers involves regular inspections to ensure they are in good working condition and effectively removing material from the conveyor belt. This includes checking for wear on the scraper blades and ensuring that they are adjusted correctly against the belt for effective cleaning. Regular maintenance not only extends the life of the scraper but also maintains the efficiency of the conveyor belt system. A proactive maintenance schedule can prevent unexpected breakdowns and reduce the need for costly repairs.
Troubleshooting Common Issues with Belt Scrapers
Common issues with belt scrapers include improper blade alignment, excessive blade wear, and inadequate pressure against the conveyor belt. Troubleshooting these issues typically involves adjusting the scraper to ensure proper contact with the belt, replacing worn blades, and checking the mounting framework for stability. Addressing these issues promptly can prevent more significant problems in the conveyor system and ensure continuous operational efficiency.
Innovations and Technological Advancements in Belt Scrapers
The field of belt scrapers is experiencing continuous innovation, with new technologies focusing on enhancing the efficiency and lifespan of scrapers. These advancements include the development of more durable materials for blades, automated adjustment features that maintain optimal pressure on the conveyor belt, and integrated monitoring systems that alert operators to scraper wear or failure. These innovations not only improve the performance of belt scrapers but also contribute to the overall automation and efficiency of conveyor systems.
Choosing the Right Belt Scraper for Your Conveyor System
Selecting the right belt scraper involves considering several factors such as the type of material being conveyed, the speed of the conveyor, and the environmental conditions of the operation. The right scraper should be robust enough to handle the specific abrasiveness of the material while being gentle enough to not damage the conveyor belt. Consulting with experts and considering customised solutions can help in selecting the ideal scraper that meets all operational requirements.
Conclusion
Belt scrapers are essential for the efficient operation of conveyor systems, providing significant benefits in terms of maintenance, safety, and operational efficiency. With proper selection, installation, and maintenance, belt scrapers can dramatically improve the functionality of conveyor systems. As technology evolves, the integration of advanced features in belt scrapers is set to further enhance their effectiveness, making them an indispensable tool in the material handling industry.
In today’s technologically advanced world, magnetic conveyor systems suppliers are integral to numerous industries, from automotive manufacturing to renewable energy production. These systems are prone to wear and tear, mechanical failures, and technological obsolescence, necessitating periodic repairs and upgrades. This comprehensive guide explores the importance of maintaining magnetic systems, identifying signs of failure, and implementing the latest technological advancements to ensure peak performance and longevity.
Understanding Magnetic Systems
High intensity magnetic separator are pivotal in numerous applications, harnessing magnetic forces to perform a variety of functions, from motion control in electric vehicles to material separation in recycling facilities. A basic understanding of these systems involves recognising the core components, such as magnets, coils, and electronic controls, which work together to create controlled magnetic fields. These fields can be used to perform work, manipulate materials, or generate energy, depending on the application. Familiarity with the operational principles of these systems is essential for anyone involved in their maintenance, repair, or upgrade.
The complexity of these systems means that they require sophisticated design and precise engineering to function correctly. As technology advances, the capabilities of these systems expand, often requiring upgrades to older systems to maintain efficiency and functionality. Keeping abreast of these advancements can significantly enhance the performance of a magnetic system and extend its operational life.
Common Failures in Magnetic Equipment
Magnetic systems, like all mechanical systems, are susceptible to a range of failures. Common issues include the degradation of magnetic materials, mechanical wear of moving parts, and electrical failures within control systems. Magnetic degradation can result from exposure to excessive heat, corrosion, or physical damage, which diminishes the strength of the magnetic field generated by the system. Mechanical wear is often seen in bearings, gears, and other moving parts, exacerbated by inadequate lubrication or alignment issues.
Electrical failures may involve short circuits, blown fuses, or failed capacitors, which are crucial for the proper functioning of electromagnetic systems. Identifying these issues early through regular inspections and maintenance routines can prevent more severe damage and costly downtime, ensuring that magnetic systems continue to operate efficiently and reliably.
Signs That Your Magnetic System Needs Repair
Recognising the signs that a Conveyor belt cleaning and repair is crucial for maintaining operational efficiency and preventing long-term damage. Early indicators include unusual noises, such as grinding or clicking, which often suggest mechanical wear or misalignment. A noticeable decrease in system performance or efficiency can also indicate that components may be failing and require attention.
Another significant sign is an increase in energy consumption, which suggests that the system is working harder to achieve the same output, often due to failing parts or suboptimal alignment. Regular monitoring of system outputs and energy usage can help identify these issues early, facilitating timely repairs that can prevent more extensive problems down the line.
Latest Advances in Magnetic Technology
The field of magnetic technology is continually evolving, with new materials, designs, and control technologies emerging regularly. Recent advancements include the development of high-temperature superconducting magnets, which offer significant energy savings and increased power density over traditional materials. Another notable development is the use of nanocrystalline magnetic materials, which provide superior strength and efficiency, allowing for smaller, more powerful systems.
Control technology has also seen significant improvements, with the advent of sophisticated software that can predict system failures before they occur and dynamically adjust parameters to optimise performance. Implementing these advanced technologies in existing systems can dramatically enhance their efficiency and longevity, making them more competitive and capable in their respective fields.
The Process of Magnetic System Evaluation
Evaluating a magnetic system’s current state is a detailed process that involves both physical inspections and performance assessments. Physical inspections focus on checking for signs of wear, corrosion, or damage to magnetic and mechanical components. Performance assessments involve testing the system’s output and efficiency, comparing them to expected levels based on specifications and historical performance data.
Advanced magnetic diagnostic tools, such as vibration analysis equipment and thermal cameras, can be used to identify issues that are not visible to the naked eye. These tools allow for a more thorough evaluation and can pinpoint specific areas that may require attention. This evaluation process is critical for determining the necessary repairs or upgrades to ensure that the system continues to operate optimally.
Key Considerations for Magnetic System Upgrades
When upgrading a magnetic system, several key considerations must be taken into account to ensure success. The primary consideration is the compatibility of new components with existing systems. This includes ensuring that electrical and mechanical interfaces match and that the new components can handle the operational demands of the system. Another important consideration is the cost of the upgrade versus the expected benefits, such as increased efficiency, reduced maintenance, and extended life expectancy.
Downtime is also a critical factor, as it can significantly impact production and operations. Planning upgrades to coincide with regular maintenance schedules or during planned downtime can minimise the impact on operations. Additionally, legal and regulatory requirements must be considered, especially if the upgrades involve significant changes to the system’s design or operation, to ensure compliance and avoid potential penalties.
DIY vs Professional Magnetic Repairs
Deciding between DIY and professional repairs for magnetic systems depends on the complexity of the system and the skill level of the in-house team. DIY repairs can be cost-effective for simple issues or for systems where in-house expertise is sufficient to perform the repairs safely and effectively. However, for more complex systems or significant repairs, professional services are recommended.
Professionals can bring specialised knowledge and experience, ensuring that repairs are done correctly and efficiently. They can also provide warranties and support that DIY repairs typically do not offer. Weighing the risks and benefits of each option is crucial, as a failed repair can result in increased damage and higher costs in the long run.
Preventive Maintenance Strategies
Implementing effective preventive maintenance strategies is essential for extending the life of magnetic systems and avoiding unplanned downtime. Regular maintenance schedules should include routine inspections, cleaning, and testing to ensure that all components are operating correctly. Predictive maintenance techniques, such as condition monitoring and performance analysis, can also be used to identify potential issues before they lead to system failure.
Training staff on proper maintenance procedures and the correct use of magnetic systems is equally important. This ensures that they can identify and address minor issues before they become major problems. A well-maintained magnetic system not only performs better but also lasts longer, providing greater value from the investment.
Optimising Magnetic Systems for Better Performance
Optimising the performance of magnetic systems involves regular reviews and adjustments to ensure they are operating at peak efficiency. This can include recalibrating magnetic fields, adjusting feed rates, or retrofitting components to improve functionality and efficiency. Using advanced software and control systems can also aid in optimisation by providing real-time data and performance metrics, allowing for dynamic adjustments.
Innovation in magnetic technology can also contribute to system optimisation. Keeping updated with the latest advancements and integrating new technologies can provide significant benefits, such as reduced energy consumption, higher outputs, and improved reliability. Continuous improvement is key to maintaining the competitiveness and effectiveness of magnetic systems in any industry.
Future Trends in Magnetic System Upgrades
The future of magnetic system upgrades is likely to see continued advancements in materials, design, and control technologies. The integration of artificial intelligence and machine learning is expected to play a significant role, providing smarter, more adaptive systems that can self-optimise and predict failures before they occur. Additionally, sustainability will become increasingly important, with a focus on energy-efficient designs and environmentally friendly materials.
As magnetic technologies evolve, staying ahead of the curve will require ongoing education and adaptation. By embracing these future trends and investing in new technologies, industries can ensure that their magnetic systems continue to provide the best possible performance, efficiency, and value.
Conclusion
Maintaining and upgrading magnetic systems is essential for any industry that relies on these critical technologies. By understanding the fundamentals of magnetic systems, recognising the signs of wear and failure, and implementing the latest advancements and maintenance strategies, businesses can ensure that their magnetic systems continue to operate effectively and efficiently. This not only enhances productivity but also extends the lifespan of the equipment, providing a competitive edge in an increasingly technological market.
In the complex world of iIndustrial metal detector conveyor Manufacturing and processing, the separation of materials plays a critical role in ensuring product quality and operational efficiency. Among the myriad technologies used for material separation, dry drum magnetic separators stand out for their effectiveness in separating ferrous materials from non-ferrous substrates. These robust machines are designed to handle large volumes of material, making them indispensable in sectors such as mining, recycling, and food processing. This guide delves into the operation, types, and strategic use of dry drum magnetic separators, providing a comprehensive overview of their functionality and benefits to modern industries.
Overview of Dry Drum Magnetic Separators
Magnetic Separators
Dry magnetic separator is engineered to facilitate the separation of ferrous metal from a variety of materials including aggregates, minerals, and granular substances. These separators consist of a stationary magnetic drum enclosed by a rotating outer shell. This design is instrumental in their ability to separate or concentrate magnetic material from the non-magnetic one. The magnetic drum attracts the ferrous material to its surface and holds it against the drum as it rotates, eventually dropping off into a separate collection area as the non-magnetic material passes freely. This mechanism not only enhances product purity but also protects processing equipment from potential damage caused by metal pieces.
The performance of dry drum magnetic separators is influenced by several factors, including the drum speed, magnetic field strength, and the feed rate of the material. Optimising these parameters is crucial to achieving the best separation efficiency. Furthermore, the design of the drum itself can vary depending on the specific needs of the operation, such as the required purity level and the physical characteristics of the material being processed. Understanding these factors is essential for anyone looking to implement this type of equipment in their operation.
Different Types of Dry Magnetic Separators
There are various magnetic separators, each designed to suit different industrial needs. The most common variants include the single drum, double drum, and triple drum designs, which increase in efficiency and capacity with the addition of each drum. Single drum separators are often used in smaller operations where the volume of material is manageable. Double and triple drum units, on the other hand, provide greater surface area and more power, making them suitable for high-capacity applications requiring higher levels of purity.
In addition to the number of drums, these separators also differ in the configuration of the magnetic system itself. Some designs employ a permanent magnet system, which is advantageous for its low maintenance and consistent performance over time. Others use an electromagnet, which allows for the adjustment of the magnetic field strength, thereby offering greater control over the separation process. Selecting the right type of dry drum magnetic separator involves understanding the specific requirements of the material handling process, including the particle size, magnetic susceptibility of the materials, and environmental conditions.
Key Applications of Dry Drum Magnetic Separators
Dry drum magnetic separators are pivotal in numerous industries where the separation of ferrous material from non-ferrous material is crucial. In the mining industry, these separators are used to enhance the purity of ores by removing ferrous contaminants, thus improving the efficiency of downstream processing and reducing wear on equipment. Similarly, in the recycling sector, they play a vital role in recovering metals from waste materials, contributing to resource conservation and profitability.
The food industry also benefits from the use of dry drum magnetic separators. They are used to remove metal contaminants from grains and other food products, thus ensuring safety and compliance with food safety standards. By preventing metal pieces from entering the final product, these separators help in maintaining the integrity and quality of food products. Overall, the versatility of dry drum magnetic separators makes them a valuable component in various production and processing lines, enhancing both safety and efficiency.
Installation Guidelines for Dry Drum Separators
Proper installation of dry drum magnetic separators is crucial for ensuring optimal performance and longevity. The installation process typically begins with a thorough site assessment, where factors such as space availability, accessibility for maintenance, and proximity to other equipment are considered. It is essential to follow the manufacturer’s instructions carefully to avoid any operational issues. Generally, the separator should be positioned at a location where the feed material is evenly distributed across the drum surface.
It is also important to ensure that the electrical and magnetic components are properly configured and tested before full-scale operation. Calibration of the magnetic field, in particular, is critical for achieving desired separation results. Regular testing and adjustments may be required to maintain optimal performance as the characteristics of the feed material or environmental conditions change. By adhering to these guidelines, operators can maximise the efficiency and lifespan of their magnetic separators.
Maintenance Tips for Longevity and Efficiency
Maintaining dry drum magnetic separators involves regular checks and routine maintenance such as magnet testing to prevent breakdowns and ensure continuous, efficient operation. Key maintenance tasks include the inspection of the magnetic drum for signs of wear and damage, checking the integrity of the belt for any cracks or tears, and verifying that the motor and gearbox are functioning smoothly. Lubrication of moving parts and the replacement of worn-out components are also crucial to prevent unexpected failures.
Moreover, the cleaning of the drum is essential to prevent the build-up of ferrous material, which can reduce the separator’s effectiveness. Implementing a regular cleaning schedule, based on the volume and type of material processed, will help maintain the performance of the separator at its peak. Additionally, keeping a log of all maintenance activities will help in tracking the health of the equipment and planning for future repairs or replacements, thereby reducing downtime and operational costs.
Common Issues and Troubleshooting
Despite best maintenance practices, operators of dry drum magnetic separators may encounter several common issues that can affect performance. One frequent problem is the decrease in separation efficiency, which can be caused by a number of factors, including incorrect drum speed, inadequate magnetic field strength, or excessive feed rate. Troubleshooting these issues typically involves adjusting the operational parameters or performing a detailed inspection of the drum and magnetic assembly.
Another common issue is the mechanical breakdown of parts such as bearings, belts, and motors. These failures can often be preempted through regular inspections and replacing parts before they fail. In cases where problems persist, consulting with the equipment manufacturer or a specialist can provide further insights and solutions to ensure that the separator returns to optimal functioning.
Performance Optimisation Techniques
To enhance the efficiency and effectiveness of dry drum magnetic separators, several performance optimisation techniques can be employed. Adjusting the magnetic field strength to suit the specific properties of the feed material is one of the most effective methods. For separators equipped with an electromagnet, this can be achieved by varying the current supplied to the coil. Adjusting the drum speed and feed rate can also significantly impact the separation quality, as these factors influence the time the material spends in the magnetic field, thereby affecting the recovery rate of ferrous metals.
Furthermore, the addition of supplementary equipment such as vibrating feeders or conveyors can improve the distribution of material over the drum, enhancing the uniformity of the separation process. Regular performance evaluations, through sampling and testing of both the feed and separated materials, will provide valuable data that can be used to fine-tune the operating parameters. These practices ensure that the dry drum magnetic separator operates at its best, delivering high-quality separation that meets industry standards.
Safety Considerations in Handling Magnetic Separators
Safety is paramount when operating any industrial equipment, and dry drum magnetic separators are no exception. The strong magnetic fields generated by these separators pose specific hazards; therefore, appropriate safety measures must be in place to protect workers. Personnel should be trained on the safe operation of the equipment, including the correct handling procedures and the use of personal protective equipment. Special attention should be given to preventing accidental contact with the magnetic drum, which can cause injuries or damage to ferromagnetic objects.
Additionally, emergency procedures should be established to address potential risks such as electrical failures or mechanical breakdowns. Regular safety audits and reviews can help ensure that all safety measures are up-to-date and effective, providing a safe working environment for all employees involved in the operation of magnetic separators.
Regulatory and Environmental Compliance
Operating dry drum magnetic separators also involves adhering to various regulatory and environmental standards. These regulations may include controls on noise levels, dust emissions, and energy consumption, all of which can impact the operation of magnetic separation equipment. Ensuring compliance not only helps in avoiding legal penalties but also promotes sustainable practices that can lead to cost savings and improved public relations.
Environmental considerations also play a crucial role, particularly in industries like mining and recycling, where waste reduction and resource recovery are vital. By optimising the operation of dry drum magnetic separators, companies can increase the recovery of valuable materials while minimising the environmental impact of their operations. This compliance not only supports regulatory adherence but also enhances the company’s reputation as a responsible and sustainable operator.
Innovations and Future Directions in Magnetic Separation
The field of magnetic separation is continuously evolving, with ongoing research and development leading to several innovative solutions that promise to enhance the efficiency and functionality of dry drum magnetic separators. These innovations include the development of stronger magnetic materials, which can provide higher magnetic fields and improve separation efficiency. Additionally, advances in computational tools are allowing for better simulation and modelling of magnetic processes, enabling the design of more efficient separators.
The integration of smart technologies, such as IoT sensors and machine learning algorithms, is also becoming more prevalent. These technologies can monitor the performance of magnetic separators in real-time, providing data that can be used to optimise operations and predict maintenance needs. As these technologies continue to advance, the future of dry drum magnetic separators looks promising, with enhancements that will further improve their efficiency, safety, and environmental compliance.
Conclusion
Dry drum magnetic separators are a cornerstone in the toolkit of many industries, facilitating the efficient and effective separation of materials. Through proper installation, routine maintenance, and adherence to safety and regulatory standards, these machines can provide years of reliable service. By staying informed of the latest developments and innovations in magnetic separation technology, businesses can ensure they are making the most of their investment and contributing to their industry’s future sustainability and success.
The world of industrial machinery is vast and varied, but few components are as crucial as the Magnetic conveyor system that drive today’s manufacturing, recycling, and mining industries. Crane magnets, magnet separators, and products from companies like Eriez Magnet have become indispensable tools in these sectors. This blog delves deep into their operations, innovations, and the integral roles they play in enhancing efficiency and safety in industrial workflows.
Understanding Crane Magnets
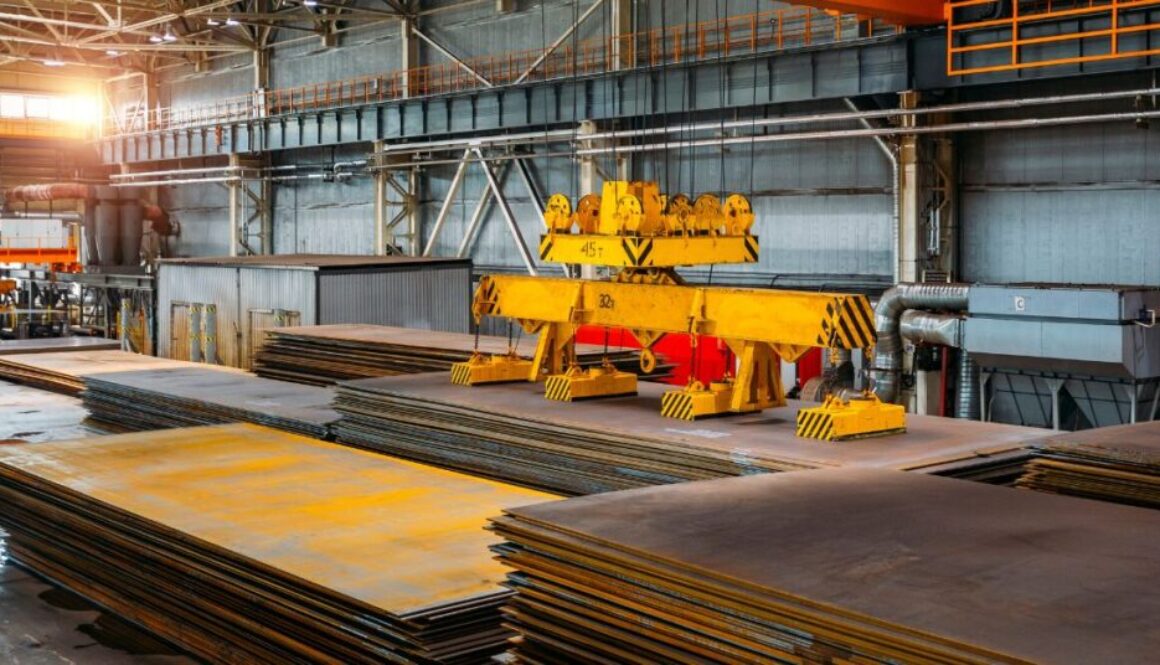
Tamp magnets are powerful magnetic devices used to move large quantities of ferromagnetic materials quickly and efficiently. They are predominantly utilised in the metal and scrap recycling industries, where large volumes of metal need to be moved or sorted. These magnets vary in design from large, round lifting magnets for heavy loads to smaller, rectangular forms tailored for specific material shapes. The technology behind these magnets is designed to maximise lifting capacity while minimising energy consumption, thereby ensuring operational efficiency and environmental responsibility.
Beyond their basic functions, crane magnets are also pivotal in maintaining workplace safety. By allowing for the remote operation of moving potentially hazardous materials, they reduce the risk of injury in environments that are fraught with potential safety hazards. Additionally, advancements in crane magnet technology have led to the development of models that can be easily integrated into automated systems, further enhancing their efficacy and reducing human exposure to dangerous conditions.
The Role of Eriez Magnet
Eriez Magnet, established in 1942, has grown to become a leader in the design and manufacture of magnetic separators, metal detection, and material handling equipment. Their products are critical in various applications across food processing, pharmaceutical, and chemical engineering industries, among others. Eriez has built a reputation for engineering excellence by providing customised solutions that meet the unique needs of their clients, ensuring that their magnetic technologies are not only effective but also tailored to specific operational requirements.
The company’s commitment to innovation is evident in its wide range of products. From overband magnets designed to automatically remove ferrous materials from conveyor belts to magnetic drum separators that ensure the purity of product lines, Eriez provides a comprehensive array of devices that cater to the complex demands of modern industries. Each product is built with the durability required to withstand the rigours of industrial environments, ensuring reliability and long-term performance.
Fundamentals of Magnet Separators
Magnet separators are critical in various industries for separating ferrous materials from non-ferrous materials, thereby facilitating significant quality control, product purification, and recovery of valuable materials. These separators function by utilising magnetic fields to attract ferrous particles while allowing other substances to pass through. This process is vital in industries such as mining, where it’s essential to extract usable metals from ores, or in recycling operations, which require the separation of recyclable ferrous metals from waste.
The design and implementation of magnetic separators involve considerations of magnetic field intensity, design of the magnetic circuit, and the operational environment. The separators must be designed to function in the specific conditions they will operate in, whether these involve high temperatures, corrosive materials, or varying levels of material throughput. The optimal functioning of these devices depends heavily on regular maintenance and calibration, which ensures that their magnetic fields remain effective over time without significant degradation.
Design and Manufacture of Industrial Magnets
When it comes to the design and manufacture of Industrial metal detector conveyor, the focus is invariably on maximising efficiency, durability, and adaptability. Engineers must consider several factors, including magnetic strength, the volume of material to be handled, and the specific environmental challenges of the installation site. Customisation of these magnets is often required to meet specific industrial needs, such as varying load capacities and operational conditions. This bespoke approach helps industries achieve their operational goals while maintaining safety and efficiency.
In addition to magnet customisation, the manufacturing process of industrial magnets involves rigorous testing and quality assurance procedures. These ensure that each magnet meets stringent standards before it is deployed in the field. The materials used in these magnets must not only possess high magnetic permeability but also be durable enough to withstand the physical stresses of continuous operation. This ensures that the magnets not only perform well but also maintain their performance over an extended period, minimising the need for frequent replacements and repairs.
Safety Protocols for Handling Industrial Magnets
Safety is paramount when dealing with industrial magnets due to their powerful magnetic fields and the heavy loads they often carry. Comprehensive training for operators is essential to ensure that all personnel are aware of the potential hazards and know how to operate magnetic equipment safely. This includes understanding how to properly activate and deactivate the magnets, as well as how to respond in the event of a malfunction.
Moreover, adherence to regulatory standards and safety protocols is not just a legal requirement but a moral imperative. Industries must ensure that all magnetic equipment is installed and maintained according to national and international safety standards. Regular inspections and audits help to identify potential risks and address them before they lead to accidents, thus safeguarding both personnel and the environment from the unintended consequences of magnetic operation failures.
Enhancements in Magnetic Technology
The landscape of magnetic technology is continually evolving, driven by advancements in materials science and magnetic theory. Recent developments have seen the introduction of superconducting magnets which offer significantly greater magnetic fields using less energy, a boon for energy-intensive industries. Similarly, the integration of IoT technology enables real-time monitoring of magnetic equipment, facilitating predictive maintenance and operational optimisation without the need for extensive manual oversight.
The future of magnetic technology looks promising, with ongoing research focusing on increasing the recyclability and energy efficiency of these systems. As the global industry moves towards more sustainable practices, magnetic technologies are expected to play a pivotal role in enabling these changes. From enhancing the purity of recycled materials to reducing the energy footprint of mining operations, the potential for innovation in the field of magnetic technology continues to expand.
Selection Criteria for Magnet Separators
Selecting the right magnet separator involves a detailed analysis of the material characteristics, process volume, and specific environmental constraints of the application. The magnetic field strength required, the type of material being processed, and the desired purity levels are all critical factors that influence the choice of separator. For instance, separators used in fine particle applications in the pharmaceutical industry require different specifications compared to those used for coarse materials in scrap metal recovery.
Understanding these variables helps in making informed decisions that can significantly impact the efficiency and cost-effectiveness of operations. Additionally, consulting with manufacturers who can provide tailored advice and solutions based on their expertise and experience with similar installations can yield better outcomes. These decisions not only affect the immediate performance of the magnetic separator but also its long-term viability and integration into larger production processes.
Maintenance and Care of Magnetic Equipment
Maintenance of Metal detector in conveyor belt magnetic equipment is critical to ensure its longevity and efficiency. Regular checks and routine maintenance tasks such as cleaning, realignment, and testing of magnetic strength are essential. This not only helps in maintaining the operational efficiency of the magnets but also in extending their lifespan, reducing the need for costly replacements.
Additionally, understanding the common issues that can affect magnetic equipment, such as demagnetisation or physical damage to the magnetic surfaces, is crucial for timely intervention. Training maintenance personnel to recognise these issues and to perform the necessary repairs can prevent prolonged downtime and ensure that the equipment continues to operate at peak performance.
Environmental Impact and Sustainability Practices
The environmental impact of magnetic technologies is an area of increasing focus. Manufacturers are now looking to reduce this impact by using more sustainable materials and manufacturing processes. This includes recycling magnetic components at the end of their lifecycle and using energy-efficient designs that reduce the power consumption of magnetic equipment.
Furthermore, the role of magnetic technologies in enhancing the sustainability of other industries, such as recycling and waste management, is significant. By improving the efficiency and effectiveness of material separation processes, these technologies not only contribute to reducing waste but also ensure that fewer resources are consumed in the production of new materials. As industries continue to seek ways to minimise their environmental footprint, the importance of innovative magnetic technologies in achieving these sustainability goals becomes ever more critical.
Conclusion
Crane magnets, Eriez Magnet, and magnet separators play indispensable roles in modern industrial operations. Their development and deployment are critical for safety, efficiency, and environmental sustainability. By understanding these tools and their applications, industries can significantly enhance their operations while also contributing to broader environmental goals. As we look to the future, the continued innovation and application of magnetic technologies will undoubtedly unlock new possibilities and drive industrial progress in numerous sectors.
In the rapidly evolving landscape of industrial technologies, magnetic separator manufacturer like crane magnets, Eriez Magnet, and magnet separators stand out due to their critical applications in several key industries. This blog aims to shed light on these technologies, focusing on their functionalities, innovations, and the advantages they offer to sectors such as recycling, mining, and manufacturing.
Essentials of Crane Magnets
Tramp magnets are powerful tools used extensively in industries that handle ferrous materials, including scrap metal yards and steel manufacturing plants. These magnets are engineered to lift heavy metal objects effortlessly, thus streamlining operations and enhancing workplace safety. The primary advantage of using crane magnets lies in their ability to handle large volumes of metal without physical contact, significantly reducing the risk of workplace accidents.
The versatility of crane magnets also allows for their integration into various machinery and equipment. From fixed electromagnets to mobile hydraulic-powered units, these magnets are adapted to meet diverse operational needs. With ongoing technological advancements, the efficiency of crane magnets continues to improve, offering higher lifting capacities and more energy-efficient designs that reduce operational costs and environmental impact.
Spotlight on Eriez Magnet
Eriez Magnet is a global leader in the design and manufacturing of magnetic separation technology. Known for their innovative solutions in processing, Eriez products are pivotal in improving product purity, protecting machinery from metal damage, and increasing process efficiency. The company’s commitment to quality and innovation is evident in their continuous development of new magnetic materials and separator designs.
Principles of Magnetic Separation
Magnetic separation is a method used to separate magnetic materials from a mixture of magnetic and non-magnetic substances. It is a straightforward yet efficient technique that is often employed in recycling, mining, and waste management. The basic principle of magnetic separation involves the use of magnets to attract magnetic materials away from non-magnetic ones, thus enabling a variety of industrial processes.
The effectiveness of magnetic separators depends on several factors including the strength of the magnets, the speed of the material flow, and the physical properties of the materials being separated. These separators are highly advantageous in industries where the quality of the end product is critical, as they help in achieving high levels of purity and efficiency in sorting and processing operations.
Innovations in Magnetic Equipment Design
Recent years have seen significant innovations in the design and function of magnetic equipment. Engineers are now incorporating advanced materials that offer stronger magnetic fields and greater durability. Additionally, the focus on smart technology has led to the development of magnetic equipment that can be remotely monitored and controlled, thus enhancing operational flexibility and reducing the need for direct human intervention.
These technological advancements not only improve the functionality of magnetic equipment but also enhance its adaptability to different industrial environments. Manufacturers are now able to offer customised solutions that are specifically designed to meet the unique challenges of their clients’ operations, ensuring optimal performance and efficiency.
Implementing Magnet Separators in Various Industries
Magnet separators are versatile tools that find applications in a myriad of industries. In the recycling industry, these separators are essential for sorting and recovering ferrous metals from waste materials, thereby increasing recycling efficiency and reducing landfill waste. In the mining sector, magnetic separators play a crucial role in extracting valuable minerals from ores, significantly enhancing the profitability and sustainability of mining operations.
Each industry presents unique challenges that require specific types of magnetic separators. For example, the food industry requires highly efficient and sanitary magnetic separators to prevent food contamination, while the pharmaceutical industry needs separators that can operate effectively at various stages of drug production. The adaptability and efficiency of magnetic separators make them invaluable across these diverse sectors.
Regulatory Framework and Compliance
The operation of magnetic equipment is subject to various regulatory standards that ensure safety, efficiency, and environmental protection. Compliance with these regulations is not only a legal requirement but also a critical factor in maintaining operational integrity and public trust. Industries using magnetic technologies must adhere to national and international standards, which typically cover aspects such as electromagnetic emissions, safety protocols, and equipment quality.
Regular audits and inspections by regulatory bodies ensure that these standards are met, helping to prevent unauthorised practices and ensuring that the equipment used is safe and reliable. This regulatory oversight is essential in maintaining high standards of operation and preventing incidents that could lead to serious operational disruptions or safety issues.
Optimisation Techniques for Magnetic Systems
Magnetic conveyor systems involves enhancing their efficiency and effectiveness through careful planning, design, and maintenance. Techniques such as adjusting the magnetic field strength, optimising the layout of the magnetic separators, and regular maintenance routines are crucial in maximising the performance of magnetic equipment.
Moreover, the integration of analytical tools and software that monitor the performance of magnetic systems in real-time can provide valuable insights into their operation. These tools help identify potential issues before they become serious problems, allowing for timely interventions that maintain the system’s efficiency and longevity.
Sustainability and Environmental Considerations
The environmental impact of magnetic technologies is increasingly becoming a focus of discussion among stakeholders in various industries. Efforts are being made to design magnetic equipment that is not only effective but also environmentally friendly. This includes reducing energy consumption, using recyclable materials, and minimising waste production during the manufacturing process.
Moreover, magnetic technologies contribute to environmental sustainability by improving the efficiency of recycling processes and reducing the need for mining new materials. By enhancing material recovery and reducing waste, these technologies play a crucial role in promoting sustainable practices across industries.
The Future of Magnetic Technology
The future of magnetic technology appears bright, with continuous advancements in materials science and magnetic applications. Researchers are exploring the potential of nanotechnology and superconducting materials to create even more powerful and energy-efficient magnetic systems. These developments promise to further revolutionise industries by providing more precise, efficient, and sustainable magnetic solutions.
The potential for magnetic technology to impact a wide range of industries cannot be understated. As research progresses and new applications are discovered, the role of magnetic technologies in driving industrial innovation and sustainability is set to grow even more significant.
Conclusion
Crane magnets, Eriez Magnet, and magnet separators are integral to the operations of many industries, offering solutions that enhance efficiency, ensure product purity, and promote environmental sustainability. Through ongoing research and development, the potential for these technologies continues to expand, promising to deliver even greater benefits to industrial processes worldwide. By embracing these advanced technologies, industries can not only improve their operational efficiency but also contribute to broader environmental and economic goals.
In the dynamic world of mining, where efficiency and productivity are paramount, the role of magnets cannot be overstated. From enhancing material handling to streamlining mineral processing, magnets play a pivotal role in various aspects of mining operations. However, to harness their full potential, it’s essential to understand the nuances of magnet repairs, training, and the different types of mining magnets available.
In this comprehensive guide, we delve into the world of mining magnets, exploring topics ranging from magnet repairs and training to overband magnets and overbelt magnetic separators. Whether you’re a seasoned professional or new to the field, this guide will equip you with the knowledge and insights needed to master the intricacies of mining magnets and optimise your mining operations. Let’s embark on a journey to unlock the power of magnets in mining.
Understanding Mining Magnets
Before delving into the intricacies of magnet repairs and magnet testing, it’s crucial to establish a foundational understanding of mining magnets. These powerful tools are indispensable in the mining industry, facilitating processes such as material handling and mineral processing with unparalleled efficiency.
At their core, mining magnets utilise magnetic fields to attract and separate ferrous materials from bulk materials, thereby enhancing operational efficiency and ensuring product purity. Among the various types of mining magnets, overband magnets and overbelt magnetic separators stand out for their versatility and effectiveness in diverse mining applications.
In the subsequent sections of this guide, we will explore the significance of proper maintenance and repair of mining magnets, the importance of comprehensive training for personnel involved in magnet operation, and the specific roles and advantages of overband magnets and overbelt magnetic separators in mining operations. By gaining a solid understanding of these foundational concepts, you’ll be better equipped to navigate the complexities of mining magnets and optimise their performance in your operations. Let’s dive deeper into the world of mining magnets and unlock their full potential.
As indispensable tools in mining operations, magnets undergo significant wear and tear over time. From routine maintenance to unexpected damages, ensuring the optimal performance of these magnets requires vigilant attention and timely repairs.
Magnet repairs encompass a range of activities aimed at addressing issues that may compromise their functionality. Common problems include damage to coils, wear on magnetic surfaces, or issues with power supply components. These issues can arise due to various factors such as harsh operating conditions, material abrasion, or simply the natural ageing of equipment.
The repair process typically begins with a thorough inspection to assess the extent of the damage and identify the root cause of the problem. Once diagnosed, repairs may involve tasks such as rewinding coils, replacing worn magnetic surfaces, or repairing electrical connections. Utilising specialised equipment and employing skilled technicians are crucial for executing repairs effectively and minimising downtime.
Regular maintenance and prompt repairs not only extend the lifespan of mining magnets but also ensure consistent performance and operational reliability. By prioritising proactive maintenance practices and investing in timely repairs, mining operators can sustain operational excellence and minimise disruptions to their production processes.
In the subsequent sections of this guide, we will delve deeper into the intricacies of magnet repairs, exploring common repair techniques, best practices for maintenance, and the importance of leveraging professional expertise in maintaining mining magnets. By understanding the critical role of repairs in sustaining operational efficiency, mining operators can optimise their magnet performance and drive continued success in their operations. Stay tuned as we uncover more insights into magnet repairs in the mining industry.
Magnet Training: Empowering Your Team
In the fast-paced and demanding environment of mining operations, the knowledge and skills of personnel are paramount to maintaining safe and efficient magnet performance. Magnet training plays a crucial role in empowering teams with the expertise needed to operate, maintain, and troubleshoot mining magnets effectively.
Comprehensive magnet training programs cover a range of essential topics, including magnet safety protocols, operational procedures, maintenance best practices, and troubleshooting techniques. By equipping personnel with the necessary knowledge and skills, training not only enhances safety but also maximises magnet efficiency, minimises downtime, and extends equipment lifespan.
One of the key aspects of magnet training is safety awareness. Operating mining magnets involves inherent risks, including exposure to high voltages, heavy machinery, and potentially hazardous materials. Proper training ensures that personnel understand and adhere to safety protocols, reducing the risk of accidents and injuries in the workplace.
Moreover, training enables personnel to optimise magnet performance by understanding the intricacies of magnet operation and maintenance. From routine inspections to troubleshooting unexpected issues, trained personnel can identify problems swiftly and implement appropriate solutions, minimising disruptions to mining operations.
Investing in magnet training demonstrates a commitment to operational excellence and employee development. By providing ongoing training opportunities, mining operators can foster a culture of continuous improvement, where personnel are empowered to enhance their skills and contribute to the overall success of the operation.
In the subsequent sections of this guide, we will delve deeper into the importance of magnet training, exploring key training topics, best practices for training implementation, and the benefits of investing in employee development. Stay tuned as we uncover more insights into how magnet training can empower your team for success in the mining industry.
Overband Magnets: Enhancing Material Handling Efficiency
In the realm of mining operations, efficient material handling is crucial for optimising productivity and ensuring the smooth flow of operations. Overband magnets and Belt metal detector emerge as indispensable tools in this regard, offering a reliable solution for removing tramp metal and enhancing material purity.
Overband magnets are positioned above conveyor belts, where they utilise magnetic fields to attract and extract ferrous materials from the conveyed material stream. This process effectively eliminates contaminants such as nails, bolts, and other metallic debris, preventing damage to downstream equipment and ensuring the quality of the end product.
The benefits of overband magnets extend beyond material purity. By removing tramp metal from the material stream, these magnets minimise the risk of costly downtime and equipment damage caused by metal contamination. Additionally, they enhance workplace safety by reducing the likelihood of accidents and injuries associated with metal debris.
Selecting the right overband magnet for specific mining applications requires careful consideration of factors such as conveyor belt width, material flow rate, and the size and composition of the conveyed material. Moreover, regular maintenance and inspection are essential to ensure optimal magnet performance and longevity.
Incorporating overband magnets into material handling systems not only improves operational efficiency but also enhances overall profitability by minimising product loss and equipment downtime. By harnessing the power of overband magnets, mining operators can streamline material handling processes and maintain a competitive edge in the industry.
In the subsequent sections of this guide, we will delve deeper into the applications, selection criteria, installation best practices, and maintenance considerations for overband magnets in mining operations. Stay tuned as we uncover more insights into how overband magnets can enhance material handling efficiency and drive success in the mining industry.
Overbelt Magnetic Separators: Streamlining Mineral Processing
In the realm of mineral processing, efficiency and accuracy are paramount for extracting valuable minerals from raw ore. conveyor magnetic separator emerge as indispensable tools in this process, offering a reliable solution for separating ferrous materials from conveyed material streams with precision and efficiency.
Overbelt magnetic separators are installed over conveyor belts, where they generate strong magnetic fields to attract and separate ferrous materials from non-ferrous materials. This separation process is crucial for ensuring the purity of the end product and minimising contamination in downstream processing equipment.
The advantages of overbelt magnetic separators extend beyond material purity. By effectively removing ferrous contaminants from the conveyed material stream, these separators minimise the risk of equipment damage and downtime caused by metal contamination. Additionally, they enhance the overall efficiency of mineral processing operations by improving the quality of the final product.
Selecting the right overbelt magnetic separator for specific mineral processing applications requires careful consideration of factors such as conveyor belt width, material composition, and processing volume. Moreover, regular maintenance and inspection are essential to ensure optimal separator performance and longevity.
Incorporating overbelt magnetic separators into mineral processing systems not only improves operational efficiency but also enhances profitability by maximising product yield and minimising waste. By harnessing the power of overbelt magnetic separators, mining operators can streamline mineral processing processes and maintain a competitive edge in the industry.
In the subsequent sections of this guide, we will delve deeper into the applications, selection criteria, installation best practices, and maintenance considerations for overbelt magnetic separators in mineral processing operations. Stay tuned as we uncover more insights into how overbelt magnetic separators can streamline mineral processing and drive success in the mining industry.
Conclusion
As we conclude our comprehensive guide to mining magnets, it’s evident that these powerful tools play a crucial role in enhancing operational efficiency, ensuring safety, and driving success in the mining industry. From magnet repairs and training to the utilisation of overband magnets and overbelt magnetic separators, every aspect of magnet management contributes to the overall effectiveness of mining operations.
Magnet repairs are essential for sustaining operational excellence, ensuring that mining magnets perform at their peak efficiency and minimising downtime. Through regular maintenance and timely repairs, mining operators can optimise magnet performance and extend equipment lifespan.
Equally important is magnet training, which empowers personnel with the knowledge and skills needed to operate, maintain, and troubleshoot mining magnets effectively. By investing in comprehensive training programs, mining operators can enhance safety, minimise disruptions, and maximise operational efficiency.
Overband magnets and overbelt magnetic separators emerge as indispensable tools for enhancing material handling efficiency and streamlining mineral processing operations. By removing ferrous contaminants from material streams, these magnets improve product purity, minimise equipment damage, and maximise product yield.
Incorporating these principles into magnet management practices not only improves operational efficiency but also enhances profitability and sustainability in the mining industry. By prioritising magnet repairs, training, and the utilisation of overband magnets and overbelt magnetic separators, mining operators can navigate the complexities of the industry with confidence and achieve lasting success.
As you embark on your journey in the world of mining magnets, remember to prioritise proactive maintenance, invest in comprehensive training, and leverage the capabilities of overband magnets and overbelt magnetic separators. By harnessing the power of mining magnets, you can optimise your operations, minimise risks, and drive success in the dynamic and challenging landscape of the mining industry.
In the bustling world of industrial operations, efficiency, safety, and precision are paramount. Among the array of tools and equipment that contribute to these essential aspects, tramp magnet stand out as indispensable assets. These magnets, including crane magnets, heavy-duty industrial magnets, and tramp magnets, play pivotal roles in various industrial settings, revolutionising the way heavy materials are handled and processed.
In this blog, we delve into the realm of lifting magnets, exploring their functionalities, applications, and significance in modern industrial processes. From their basic principles to their advanced applications, we aim to provide a comprehensive understanding of how lifting magnets contribute to enhancing productivity, ensuring safety, and maintaining the integrity of industrial operations. So, let’s embark on a journey to uncover the magnetic forces that power the industrial world.
Understanding Lifting Magnets
In the intricate dance of industrial operations, tramp metal magnets serve as silent yet powerful partners, seamlessly integrating into workflows to handle heavy loads with ease and precision. Understanding the intricacies of lifting magnets is crucial to harnessing their full potential and optimising their use in various industrial settings.
Definition and Function of Lifting Magnets:
Lifting magnets, also known as magnetic lifters, are devices designed to lift and move heavy ferrous materials using magnetic force.
These magnets typically consist of a magnetic circuit, including one or more magnets, encased in a durable housing.
The magnetic circuit generates a strong magnetic field, attracting ferrous materials and securely holding them in place during lifting and transportation.
Different Types of Lifting Magnets Available:
Permanent Lifting Magnets: These magnets utilise permanent magnets, such as neodymium or ferrite, to create a magnetic field without the need for external power.
Electro Lifting Magnets: These magnets use an electromagnetic coil powered by electricity to generate a magnetic field, offering greater control over lifting capacity and magnetisation.
Battery-Powered Lifting Magnets: A variation of electro lifting magnets, these devices are powered by rechargeable batteries, providing portability and flexibility in various industrial settings.
Applications of Lifting Magnets in Various Industries:
Manufacturing: Lifting magnets are commonly used in metal fabrication, steel mills, and automotive manufacturing for lifting and transporting raw materials, finished products, and components.
Construction: In construction sites, lifting magnets facilitate the handling of steel beams, pipes, and other heavy materials, streamlining construction processes and enhancing efficiency.
Recycling: Lifting magnets play a crucial role in recycling facilities by efficiently sorting and handling ferrous materials such as scrap metal and discarded appliances.
By understanding the different types of lifting magnets and their applications, industries can leverage these versatile tools to streamline operations, improve productivity, and ensure the safe handling of heavy materials. In the next section, we will explore the specialised realm of crane magnets and their unique functionalities in industrial lifting operations.
Exploring Crane Magnets
Within the bustling landscape of industrial operations, crane magnets emerge as specialised tools designed to handle heavy loads with precision and efficiency. As integral components of crane systems, these magnets offer unique functionalities tailored to the demands of lifting and transporting ferrous materials in diverse industrial settings.
Definition and Purpose of Crane Magnets:
Crane magnets, also known as magnetic crane attachments or Suspended electromagnet, are specialised devices mounted on cranes or hoists to facilitate the lifting and transportation of ferrous materials.
These magnets utilise electromagnetic principles to generate a powerful magnetic field, enabling them to attract and securely hold ferrous objects during lifting operations.
The primary purpose of crane magnets is to enhance the efficiency, safety, and precision of material handling processes in industries such as construction, manufacturing, and recycling.
How Crane Magnets Differ from Other Lifting Magnets:
Unique Design: Crane magnets are specifically designed to be mounted on cranes or hoists, allowing for easy integration into existing material handling systems.
Electromagnetic Operation: Unlike permanent lifting magnets, crane magnets rely on electromagnetic coils powered by electricity to generate a magnetic field, providing greater control over magnetisation and lifting capacity.
Versatile Applications: Crane magnets are versatile tools capable of handling a wide range of ferrous materials, including steel plates, beams, pipes, and scrap metal, making them indispensable in industries where heavy lifting is routine.
Examples of Industries and Scenarios Where Crane Magnets are Commonly Used:
Steel Industry: In steel mills and metal fabrication facilities, crane magnets are used to lift and transport steel coils, sheets, and billets with precision and efficiency, minimising manual handling and reducing the risk of accidents.
Construction Sites: On construction sites, crane magnets facilitate the handling of steel beams, columns, and other structural components, accelerating construction processes and improving productivity.
Recycling Facilities: In recycling facilities, crane magnets play a crucial role in sorting and processing ferrous materials such as scrap metal and discarded appliances, streamlining recycling operations and maximising resource recovery.
By exploring the unique functionalities and applications of crane magnets, industries can gain insights into how these specialised tools can optimise material handling processes, improve workflow efficiency, and ensure the safe and effective transportation of heavy ferrous materials. In the next section, we will delve into the realm of heavy-duty industrial magnets and their diverse capabilities in industrial applications.
Heavy-Duty Industrial Magnets: A Closer Look
In the intricate tapestry of industrial operations, heavy-duty industrial magnets stand out as robust and versatile tools capable of exerting powerful magnetic forces to handle a wide range of ferrous materials. These magnets, engineered for durability and reliability, play a vital role in various industrial applications, offering unmatched capabilities for material handling, separation, and processing.
Overview of Heavy-Duty Industrial Magnets and Their Capabilities:
Heavy-duty Industrial metal detector conveyor are designed to withstand the rigours of industrial environments, including high temperatures, abrasive materials, and heavy loads.
These magnets utilise advanced magnetic materials and engineering principles to generate strong magnetic fields, enabling them to attract, hold, and manipulate ferrous materials with precision and efficiency.
From lifting and transporting heavy loads to separating and sorting ferrous contaminants, heavy-duty industrial magnets offer diverse capabilities to meet the demands of industrial processes across different sectors.
Types of Heavy-Duty Industrial Magnets Available and Their Specifications:
Electromagnets: These magnets use electrical currents to generate magnetic fields, providing adjustable lifting capacities and precise control over magnetisation.
Permanent Magnets: Made from materials such as neodymium, samarium cobalt, or ferrite, permanent magnets offer continuous magnetic power without the need for external power sources.
Magnetic Separators: These specialised magnets are designed to remove unwanted ferrous contaminants from materials during processing, ensuring product quality and equipment integrity.
Real-World Examples Showcasing the Effectiveness of Heavy-Duty Industrial Magnets:
Steel Industry: In steel mills and metal fabrication facilities, electromagnets are used to lift and transport heavy steel coils, ingots, and billets, optimising material handling processes and improving operational efficiency.
Mining Operations: Magnetic separators play a crucial role in mining operations by removing ferrous contaminants from mined materials, preventing damage to downstream processing equipment and enhancing ore quality.
Food Processing: In food processing plants, magnetic separators are employed to remove ferrous contaminants from raw materials and finished products, ensuring compliance with food safety standards and safeguarding consumer health.
By examining the diverse capabilities and real-world applications of heavy-duty industrial magnets, industries can gain insights into how these advanced tools can optimise material handling processes, enhance product quality, and ensure the integrity of industrial operations. In the next section, we will explore the specialised realm of tramp magnets and their crucial role in maintaining product quality and equipment integrity.
The Role of Tramp Magnets in Industrial Processes
In the intricate landscape of industrial processes, the presence of unwanted ferrous contaminants, known as tramp metal, can pose significant challenges to product quality, equipment integrity, and overall operational efficiency. Tramp magnets emerge as specialised tools designed to address these challenges by effectively capturing and removing ferrous contaminants from materials during processing, ensuring the purity and integrity of the end product.
Explanation of Tramp Magnets and Their Importance in Industrial Settings:
Tramp magnets, also referred to as magnetic separators or magnetic traps, are devices specifically designed to capture and remove ferrous contaminants, such as metal shavings, bolts, screws, and nails, from materials flowing through industrial processing systems.
These magnets utilise powerful magnetic fields to attract and hold ferrous contaminants, preventing them from contaminating downstream equipment, damaging product quality, or causing safety hazards.
The importance of tramp magnets in industrial settings lies in their ability to maintain product purity, ensure equipment integrity, and comply with regulatory standards for product quality and safety.
How Tramp Magnets Contribute to the Removal of Unwanted Metallic Contaminants:
Magnetic Separation: Tramp magnets employ magnetic separation principles to capture and remove ferrous contaminants from materials passing through processing equipment, such as conveyors, chutes, and pipelines.
Efficient Capture and Retention: These magnets feature high-strength magnetic circuits designed to efficiently capture and retain ferrous contaminants, ensuring thorough removal and preventing recontamination of processed materials.
Easy Maintenance and Cleaning: Tramp magnets are engineered for easy maintenance and cleaning, allowing operators to periodically remove captured contaminants and maintain peak performance without disrupting production processes.
Case Studies Illustrating the Benefits of Tramp Magnets in Industrial Operations:
Metalworking Industry: In metalworking operations, tramp magnets are installed in cutting, grinding, and machining equipment to capture metal chips and debris, preventing damage to precision tools and ensuring the quality of machined parts.
Food Processing Plants: In food processing plants, tramp magnets are employed to remove ferrous contaminants from raw materials, such as grains, powders, and liquids, safeguarding product purity and compliance with food safety regulations.
Recycling Facilities: Tramp magnets play a crucial role in recycling facilities by capturing ferrous contaminants from recyclable materials, such as plastic, glass, and paper, ensuring the quality of recycled products and maximising resource recovery.
By understanding the importance of tramp magnets and their role in industrial processes, industries can implement effective contamination control strategies, safeguard product quality, and optimise operational efficiency. In the next section, we will delve into safety considerations and best practices for the proper installation, operation, and maintenance of lifting magnets and related equipment.
Conclusion
In the dynamic realm of industrial operations, lifting magnets emerge as indispensable tools that revolutionise material handling processes, enhance efficiency, and ensure safety. From the versatile capabilities of crane magnets to the robust performance of heavy-duty industrial magnets and the essential role of tramp magnets in contamination control, these magnetic solutions play a vital role in diverse industries worldwide.
Throughout this exploration, we have delved into the fundamentals of lifting magnets, understanding their functionalities, applications, and significance in modern industrial settings. We’ve examined how crane magnets facilitate precision lifting operations, how heavy-duty industrial magnets optimise material handling processes, and how tramp magnets safeguard product quality and equipment integrity.
Moreover, we’ve highlighted the importance of prioritising safety when using lifting magnets, emphasising the need for adherence to safety protocols, proper installation, operation, and maintenance practices, and compliance with regulatory standards. By following these guidelines, industries can create a safe working environment, protect personnel, and ensure the integrity of materials being handled.
As we conclude this journey into the world of lifting magnets, it’s evident that these magnetic solutions are more than just tools; they are catalysts for innovation, efficiency, and safety in industrial operations. By harnessing the power of lifting magnets and embracing best practices for their use, industries can unlock new possibilities, streamline processes, and achieve greater success in today’s competitive landscape. So, let us continue to harness the magnetic forces that propel us forward, shaping a future where safety, efficiency, and excellence reign supreme in industrial endeavours.
In the intricate tapestry of industrial processes, the art of separation holds a pivotal role. From mining to recycling, food processing to waste management, the ability to isolate and extract desired elements or materials is indispensable. At the heart of this capability lies the magnetic drum separator—an ingenious device that wields the forces of magnetism to accomplish feats of separation with precision and efficiency.
In this blog, we embark on a journey into the realm of magnetic drum separators, exploring their inner workings, practical applications, and the transformative impact they have across various industries. We delve into the nuanced world of dry drum magnetic separators, shedding light on their significance, advantages, and the considerations that guide their selection. Join us as we uncover the magic woven into the fabric of industrial separation processes and discover the profound role that magnetic drum separators play in shaping the landscape of modern industry.
Understanding Magnetic Drum Separators
Magnetic drum separators are marvels of engineering designed to harness the power of magnetism for efficient separation in industrial processes. In this section, we will delve deeper into the workings of these ingenious devices, exploring their fundamental principles and the different types that exist.
Definition and Basic Functionality
At its core, a magnetic separator is a cylindrical drum containing powerful magnets arranged in a specific configuration. These magnets generate a magnetic field that attracts and holds ferrous materials, such as iron and steel, while allowing non-magnetic materials to pass through. As materials flow through the drum, the magnetic field effectively separates the ferrous contaminants, resulting in purified output streams.
How Magnetic Drum Separators Work
The operation of magnetic drum separators relies on the principles of magnetism and motion. When materials are fed into the drum, they come into contact with the magnetic field generated by the magnets inside the drum. Ferrous particles within the material are attracted to the magnets and cling to the drum’s surface, while non-magnetic particles continue their trajectory, eventually exiting the drum as a clean product.
Different Types: Wet Drum vs. Dry Drum Separators
Two primary variants of magnetic drum separators exist: wet drum separators and dry drum separators. Wet drum separators utilise water or other liquid mediums to facilitate the separation process, making them ideal for applications where moisture is present or where a higher degree of separation efficiency is required. On the other hand, dry drum separators operate without the need for a liquid medium, offering advantages such as lower operating costs and reduced maintenance requirements.
Applications Across Industries
The versatility of magnetic drum separators makes them indispensable in a wide range of industries. From mining and mineral processing to recycling and food manufacturing, these separators find applications wherever the need for efficient separation of ferrous contaminants arises. They play a vital role in ensuring product quality, maintaining equipment integrity, and adhering to regulatory standards across diverse industrial settings.
In the subsequent sections, we will delve deeper into the realm of dry drum magnetic separators, exploring their unique features, benefits, and real-world applications. Join us as we unravel the mysteries of these remarkable devices and uncover the myriad ways in which they contribute to the efficiency and sustainability of industrial processes.
Exploring Dry Drum Magnetic Separators
Dry type magnetic separator represent a pinnacle of innovation in the field of industrial separation technology. In this section, we delve into the intricacies of these remarkable devices, uncovering their unique features, advantages, and the diverse applications that make them indispensable in numerous industries.
Definition and Purpose
Dry drum magnetic separators are sophisticated devices designed to efficiently separate ferrous materials from non-magnetic substances in dry environments. Unlike their wet counterparts, which rely on liquid mediums for separation, dry drum separators operate without the need for moisture, making them ideal for applications where water is scarce or where dry processing is preferred.
Advantages of Dry Drum Magnetic Separators
Dry drum magnetic separators offer a host of advantages over alternative separation methods, making them increasingly popular in industrial settings. Some key benefits include:
Reduced Operating Costs: Dry drum separators eliminate the need for costly liquid mediums, resulting in lower operational expenses and greater cost-effectiveness.
Enhanced Efficiency: By operating in dry environments, these separators minimise the risk of material clumping or clogging, ensuring consistent and efficient separation performance.
Versatility: Dry drum separators are adaptable to a wide range of materials and processing conditions, making them suitable for diverse applications across industries.
Environmental Sustainability: The absence of liquid mediums in dry drum separators reduces environmental impact and simplifies waste management, aligning with sustainability goals.
Key Features and Components
Dry drum magnetic separators comprise several key components, each playing a crucial role in the separation process. These may include:
Magnetic Drum: The heart of the separator, containing powerful magnets arranged to generate a magnetic field capable of attracting and capturing ferrous contaminants.
Feeder: Responsible for introducing material into the separator, ensuring a steady flow for optimal separation efficiency.
Conveyor Belt: Transports material through the separator, facilitating interaction with the magnetic field and enabling effective separation.
Discharge Chute: Directs separated materials into appropriate collection points, ensuring clean product streams and minimising contamination risks.
Examples of Industries Utilising Dry Drum Magnetic Separators
Dry drum magnetic separators find application in a myriad of industries, including:
Mining and Mineral Processing: Used to extract and purify valuable minerals from ore streams, enhancing productivity and product quality.
Recycling: Employed to remove ferrous contaminants from recyclable materials, improving material purity and recycling efficiency.
Food Processing: Utilised to ensure food safety by removing metal contaminants from raw materials and finished products.
Plastics Recycling: Applied to separate ferrous materials from plastic waste streams, enabling efficient recycling and resource recovery.
In the subsequent sections, we will delve deeper into the benefits and considerations associated with dry drum magnetic separators, as well as explore real-world applications and case studies highlighting their effectiveness in various industries. Join us as we continue our journey into the realm of industrial separation technology, uncovering the transformative potential of dry drum magnetic separators.
Benefits of Dry Drum Magnetic Separators
Dry drum magnetic separators stand as a testament to innovation and efficiency in the realm of industrial separation technology. In this section, we explore the multitude of benefits offered by these sophisticated devices, shedding light on their transformative impact on industrial processes and operations.
Efficiency in Removing Magnetic Contaminants
One of the primary advantages of dry drum magnetic separators is their exceptional efficiency in removing ferrous contaminants from material streams. The powerful magnetic field generated within the separator attracts and captures even the smallest magnetic particles, ensuring thorough and effective separation. This capability translates to cleaner product streams, improved product quality, and enhanced overall process efficiency.
Reduced Maintenance Requirements
Unlike wet drum separators, which necessitate regular maintenance to manage liquid mediums and prevent corrosion, dry drum magnetic separators operate in dry environments, significantly reducing maintenance requirements. The absence of liquid components minimises the risk of equipment corrosion and simplifies upkeep, resulting in lower maintenance costs and increased uptime for industrial operations.
Cost-Effectiveness Compared to Alternative Methods
Dry drum magnetic separators offer a cost-effective solution for industrial separation needs, particularly in applications where water-based methods may be impractical or costly. By eliminating the need for liquid mediums and associated infrastructure, these separators reduce operational expenses and capital investments, providing a favourable return on investment over the long term. Additionally, the efficiency and reliability of dry drum separators contribute to further cost savings by minimising product losses and maximising resource utilisation.
Environmental Benefits
The environmental sustainability of dry drum magnetic separators is another significant advantage. By operating without the use of water or chemicals, these separators minimise environmental impact and reduce resource consumption. Furthermore, the clean and efficient separation achieved by dry drum separators helps industries comply with environmental regulations and sustainability standards, contributing to overall environmental stewardship and responsible resource management.
Enhanced Safety
Dry drum magnetic separators promote workplace safety by minimising the risk of accidents and hazards associated with handling liquid mediums. The absence of water eliminates slip and fall hazards, reduces the potential for chemical exposure, and enhances overall safety in industrial environments. Additionally, the efficient removal of ferrous contaminants ensures product integrity and safety, particularly in industries such as food processing where product quality is paramount.
In conclusion, the benefits of dry drum magnetic separators are multifaceted and far-reaching, encompassing efficiency, cost-effectiveness, environmental sustainability, and safety. These innovative devices continue to change industrial separation processes, offering a reliable and efficient solution for diverse applications across industries. In the subsequent sections, we will explore real-world applications and case studies that illustrate the practical impact of dry drum magnetic separators in various industrial settings. Join us as we continue our exploration of these transformative technologies and their role in shaping the future of industrial separation.
Considerations for Choosing a Dry Drum Magnetic Separator
Selecting the right dry drum magnetic separator is essential to ensuring optimal performance, efficiency, and cost-effectiveness in industrial separation applications. In this section, we delve into key considerations that guide the selection process, providing insights into factors that influence separator performance, maintenance requirements, and overall suitability for specific industry needs.
Factors to Consider in Selecting the Right Separator
Magnetic Strength and Configuration: The magnetic strength and configuration of the separator’s magnets play a crucial role in determining its separation efficiency and effectiveness in capturing ferrous contaminants. Higher magnetic strengths and optimised magnet configurations result in improved separation performance and higher purity of the final product.
Particle Size and Composition: Consideration must be given to the particle size and composition of the materials being processed. Some dry drum magnetic separators are better suited for fine particle separation, while others may be more effective for coarse particle separation. Understanding the size distribution and composition of the material stream is essential for selecting a separator that can achieve the desired separation outcomes.
Material Flow Rate and Throughput: The material flow rate and throughput requirements of the application should be carefully evaluated to ensure that the selected separator can handle the anticipated volume of material effectively. Choosing a separator with appropriate dimensions, conveyor speed, and processing capacity is essential for maintaining optimal separation efficiency and preventing bottlenecks in the production process.
Operating Environment and Conditions: Consideration must be given to the operating environment and conditions in which the separator will be deployed. Factors such as temperature, humidity, dust levels, and exposure to corrosive substances can impact the performance and longevity of the separator. Selecting a separator with durable construction materials, corrosion-resistant components, and appropriate sealing mechanisms is essential for ensuring reliable operation in challenging environments.
Maintenance and Operational Considerations
Ease of Maintenance: The ease of maintenance and accessibility of critical components such as the magnetic drum, conveyor belt, and discharge chute should be considered when selecting a dry drum magnetic separator. Choosing a separator with user-friendly maintenance features, such as quick-release mechanisms and accessible inspection ports, can simplify maintenance tasks and reduce downtime.
Wear and Abrasion Resistance: Dry drum magnetic separators are subjected to significant wear and abrasion during operation, particularly in applications involving abrasive materials or high material velocities. Selecting a separator with wear-resistant liners, hardened surfaces, and robust construction materials can prolong the service life of the separator and minimise maintenance requirements.
Cleaning and Decontamination Procedures: Consideration must be given to the cleaning and decontamination procedures required to maintain separator performance and prevent cross-contamination between material streams. Selecting a separator with easy-to-clean surfaces, removable components, and effective cleaning mechanisms can streamline cleaning procedures and ensure compliance with hygiene and safety standards.
Cost Analysis and Return on Investment
Initial Investment Cost: The initial investment cost of the separator, including purchase price, installation, and commissioning expenses, should be carefully evaluated in relation to the expected benefits and outcomes. While higher-quality separators may command a higher upfront cost, they may offer superior performance, reliability, and longevity, resulting in a favourable return on investment over the long term.
Operating and Maintenance Costs: Consideration must be given to the ongoing operating and maintenance costs associated with the separator, including energy consumption, consumables, spare parts, and labour expenses. Choosing a separator with low operating and maintenance costs can help minimise total cost of ownership and maximise profitability over the lifespan of the equipment.
Return on Investment: A comprehensive cost-benefit analysis should be conducted to assess the potential return on investment (ROI) associated with the selected separator. Factors such as increased productivity, improved product quality, reduced waste, and compliance with regulatory standards should be taken into account when evaluating the ROI of the separator.
Safety and Regulatory Compliance
Safety Features: The safety features and compliance of the separator with relevant industry standards and regulations should be carefully evaluated to ensure the safety of personnel and compliance with legal requirements. Selecting a separator with safety interlocks, guarding, emergency stop systems, and other safety features can help minimise the risk of accidents and ensure safe operation in industrial environments.
Regulatory Compliance: Dry drum magnetic separators used in specific industries, such as food processing, may be subject to regulatory requirements and standards governing equipment design, construction, and hygiene. Selecting a separator that meets or exceeds relevant regulatory requirements can help ensure compliance with industry standards and facilitate regulatory approval for the equipment.
Conclusion
In the intricate tapestry of industrial processes, the role of separation stands as a cornerstone, dictating the efficiency, quality, and sustainability of countless operations. At the forefront of this endeavour are dry drum magnetic separators—sophisticated devices that harness the power of magnetism to achieve unparalleled levels of separation efficiency and reliability.
Throughout this exploration, we’ve delved into the inner workings, benefits, considerations, and applications of dry drum magnetic separators, uncovering their transformative potential across diverse industries and settings. From mining and recycling to food processing and plastics recycling, these innovative devices have proven indispensable, enabling businesses to enhance productivity, ensure product quality, and meet stringent regulatory standards.
The advantages of dry drum magnetic separators are myriad, encompassing efficiency in removing magnetic contaminants, reduced maintenance requirements, cost-effectiveness, environmental sustainability, and enhanced safety. By selecting the right separator and carefully evaluating factors such as magnetic strength, particle size, material flow rate, operating environment, maintenance requirements, cost considerations, safety features, and regulatory compliance, businesses can achieve optimal separation performance, efficiency, and cost-effectiveness, driving productivity, profitability, and competitiveness in their respective industries.
As we look to the future, the potential for innovation and advancement in the field of industrial separation technology is boundless. From the development of novel materials and configurations to the integration of intelligent monitoring and control systems, the evolution of dry drum magnetic separators holds promise for further enhancing separation efficiency, reducing environmental impact, and unlocking new possibilities for industrial processes.
In closing, dry drum magnetic separators stand as testament to human ingenuity and innovation, embodying the relentless pursuit of excellence in industrial separation technology. As businesses continue to seek ways to optimise their processes, minimise environmental footprint, and meet evolving market demands, the role of dry drum magnetic separators will only grow in significance, shaping the landscape of industrial separation for generations to come. Join us on this journey of exploration and discovery as we continue to push the boundaries of what’s possible in industrial separation, guided by the enduring principles of efficiency, sustainability, and excellence.
In the bustling landscape of modern industry, magnetic conveyor system stand as indispensable arteries, tirelessly moving materials and products along their designated paths. From manufacturing plants to distribution centres, these intricate networks of belts and rollers ensure the smooth flow of goods, optimising efficiency and productivity. However, amidst the ceaseless motion, there exists a critical imperative: the need for thorough conveyor belt cleaning and vigilant metal detection.
The integrity of conveyor systems hinges not only on their ability to transport goods but also on their capacity to maintain cleanliness and detect any unwanted contaminants. In this introductory exploration, we embark on a journey through the realms of conveyor belt cleaning and metal detection, uncovering the vital role they play in safeguarding product quality, operational efficiency, and, above all, the safety of both consumers and workers. Let us delve into the essential components, manufacturers, and best practices that comprise this integral facet of industrial operations, illuminating the path toward optimal performance and peace of mind.
Understanding Conveyor Belt Cleaning
Metal Detection
Within the dynamic ecosystem of industrial operations, cleanliness stands as a cornerstone of efficiency and safety. Conveyor belt cleaning is not merely a matter of aesthetics; it is a fundamental requirement for maintaining optimal performance and preventing contamination. As materials traverse conveyor belts, they leave behind residues, debris, and potential contaminants, which can compromise product quality and pose risks to consumer health. Consequently, various methods of conveyor belt cleaning have emerged, each tailored to address specific challenges and operational needs. Mechanical methods, such as scrapers and brushes, physically remove debris from belt surfaces, ensuring smooth and unimpeded movement. Chemical cleaning agents may also be employed to dissolve stubborn residues and sanitise conveyor components, particularly in industries with stringent hygiene standards.
Moreover, proactive maintenance and adherence to cleaning schedules are paramount. Regular inspections allow operators to identify potential issues early on, preventing the accumulation of debris and minimising the risk of costly downtime. By embracing a comprehensive approach to conveyor belt cleaning, businesses can uphold the highest standards of product integrity, operational efficiency, and regulatory compliance.
The Role of Metal Detection in Conveyor Systems
In the intricate dance of industrial production, the presence of foreign objects poses a persistent threat to product quality and consumer safety. This is where metal detection in conveyor systems emerges as a guardian, diligently scanning for any unwanted intruders that may have found their way into the production line.
Metal detectors integrated into conveyor systems serve as vigilant sentinels, employing advanced technology to identify and isolate metal contaminants with precision and accuracy. Whether it’s a stray bolt in a batch of food products or a metallic shard in pharmaceuticals, these detectors swiftly alert operators to the presence of foreign materials, allowing for prompt removal and mitigation of potential hazards.
The applications of metal detection span a wide spectrum of industries, from food processing and packaging to pharmaceuticals, mining, and beyond. In each of these domains, the integrity of products is non-negotiable, and the consequences of contamination can be dire. By harnessing the power of metal detection technology within conveyor systems, businesses can fortify their defences against potential threats, safeguarding product quality, brand reputation, and, most importantly, consumer trust.
In the next section, we’ll delve into the landscape of conveyor belt metal detector manufacturers, exploring the key considerations and criteria for selecting the right partner in this critical endeavour. Stay tuned as we navigate the realm of innovation and excellence in metal detection technology.
Conveyor Belt Metal Detector Manufacturers: Choosing the Right Partner
In the realm of conveyor belt metal detection, the choice of manufacturer is a pivotal decision that can profoundly impact the effectiveness and reliability of your detection system. With a myriad of manufacturers vying for attention in the market, selecting the right partner demands careful consideration of various factors to ensure optimal performance and seamless integration within your operational environment.
Expertise and Reputation: Begin your quest by researching the track record and reputation of potential manufacturers. Look for companies with a proven history of excellence in metal detection technology and a strong reputation for reliability and customer satisfaction. Testimonials, case studies, and industry awards can offer valuable insights into a manufacturer’s credentials and capabilities.
Product Range and Customisation: Assess the breadth and depth of each manufacturer’s product range, paying close attention to their ability to tailor solutions to your specific requirements. Consider factors such as conveyor size, material composition, throughput rates, and detection sensitivity levels. Opt for manufacturers capable of delivering customised solutions that align seamlessly with your operational needs.
Technology and Innovation: Stay abreast of the latest advancements and innovations in metal detection technology, and seek out manufacturers at the forefront of these developments. Look for features such as multi-frequency detection, advanced signal processing algorithms, and integration with automation and data analytics systems. Choosing a manufacturer at the cutting edge of technology ensures future-proofing and longevity for your detection system.
Compliance and Certification: Ensure that any manufacturer under consideration adheres to relevant industry standards and regulations governing metal detection equipment. Look for certifications such as ISO 9001 for quality management systems and ISO 22000 for food safety management systems. Compliance with regulatory requirements demonstrates a commitment to quality, safety, and best practices.
Customer Support and Service: Evaluate the level of customer support and service offered by each manufacturer, including pre-sales consultant, installation assistance, training programs, and ongoing technical support. Choose manufacturers known for their responsiveness, expertise, and dedication to customer satisfaction. A reliable support network is essential for maximising the performance and longevity of your detection system.
By carefully weighing these factors and conducting thorough due diligence, you can confidently select a conveyor belt metal detector manufacturer that meets your needs and exceeds your expectations. In the next section, we’ll delve into the operational advantages and applications of conveyor belt separators and magnetic separators, complementing the capabilities of metal detection systems in ensuring product integrity and safety. Stay tuned for insights into these indispensable components of conveyor system management.
Conveyor Belt Separators and Magnetic Separators
In the intricate ecosystem of conveyor systems, maintaining product integrity and preventing contamination are paramount objectives. Conveyor belt separators and magnetic separators emerge as indispensable tools in achieving these goals, offering effective solutions for the removal of ferrous and non-ferrous materials from conveyed products.
Conveyor Belt Separators: These specialised devices are designed to intercept and divert contaminants that may be present on conveyor belts, preventing them from reaching downstream processes or contaminating finished products. Conveyor belt separators come in various configurations, including magnetic, pneumatic, and gravity-based systems, each offering unique advantages depending on the application and material characteristics.
Magnetic Separators: Among the most widely used and effective separators are magnetic systems, which harness the power of magnets to attract and remove ferrous contaminants from conveyed materials. Suspended over conveyor belts or positioned within chutes, magnetic separators efficiently capture and retain ferrous particles, ensuring product purity and preventing damage to downstream equipment.
Applications and Benefits: Conveyor belt separators and magnetic separators find applications across a diverse range of industries, including mining, aggregate processing, recycling, food processing, and manufacturing. Whether it’s removing metal contaminants from bulk materials, segregating recyclable materials, or ensuring product purity in food and pharmaceutical production, these separators play a critical role in maintaining operational efficiency and product quality.
Types of Magnetic Separators: Magnetic separators come in various configurations to suit different applications and material handling requirements. Common types include suspended magnets, magnetic pulleys, magnetic drums, and magnetic plates. Each type offers specific benefits in terms of efficiency, ease of installation, and adaptability to different conveyor configurations.
Integration with Metal Detection Systems: For comprehensive contaminant detection and removal, magnetic separators are often integrated with metal detection systems within conveyor systems. This synergistic approach ensures a multi-layered defence against both ferrous and non-ferrous contaminants, enhancing product purity and minimising the risk of costly recalls or product rejection.
By incorporating conveyor belt separators and magnetic separators into their operations, businesses can mitigate the risk of product contamination, enhance operational efficiency, and safeguard product quality and consumer safety. In the subsequent section, we’ll explore the seamless integration of conveyor belt cleaning, metal detection, and separation technologies, providing a holistic approach to conveyor system management. Stay tuned as we delve deeper into the synergy of these essential components and their collective impact on industrial operations.
Integrating Conveyor Belt Cleaning and Metal Detection Systems
In the dynamic landscape of industrial operations, the synergy of conveyor belt cleaning, metal detection, and separation technologies offers a comprehensive approach to ensuring product integrity, operational efficiency, and regulatory compliance. By seamlessly integrating these essential components within conveyor systems, businesses can establish a multi-layered defence against contaminants, safeguarding both product quality and consumer safety.
Holistic Contaminant Management: The integration of conveyor belt cleaning systems, metal detectors, and magnetic dirt separator forms a holistic approach to contaminant management throughout the production process. From the moment raw materials enter the conveyor system to the final packaging of finished products, each component plays a vital role in detecting, removing, and preventing contaminants from compromising product quality.
Early Detection and Prevention: Metal detection systems serve as the first line of defence, detecting and alerting operators to the presence of metal contaminants as materials traverse the conveyor belt. By identifying potential threats early on, businesses can take proactive measures to prevent contamination, such as stopping the conveyor line for inspection or diverting affected materials for further analysis.
Effective Contaminant Removal: Conveyor belt cleaning systems ensure that conveyor surfaces remain free from debris, residues, and potential contaminants that may accumulate during the production process. By regularly cleaning conveyor belts, businesses minimise the risk of cross-contamination and maintain optimal operational efficiency.
Precision Separation: Magnetic separators complement metal detection systems by effectively capturing and removing ferrous contaminants from conveyed materials. Whether suspended over conveyor belts or positioned within processing equipment, magnetic separators offer precise separation capabilities, ensuring product purity and protecting downstream equipment from damage.
Streamlined Integration: Modern conveyor systems are designed to facilitate the seamless integration of cleaning, detection, and separation technologies. Advanced control systems and automation solutions enable real-time monitoring of conveyor operations, allowing for rapid response to detected contaminants and ensuring uninterrupted production flow.
Regulatory Compliance and Consumer Confidence: By implementing a comprehensive approach to contaminant management, businesses demonstrate their commitment to regulatory compliance and consumer safety. Adhering to industry standards and best practices not only mitigates the risk of product recalls and liability but also enhances consumer confidence in the quality and safety of their products.
By embracing the synergy of conveyor belt cleaning, metal detection, and separation technologies, businesses can fortify their defences against contaminants, enhance operational efficiency, and uphold the highest standards of product quality and safety. In the subsequent section, we’ll delve into best practices for conveyor belt maintenance, offering insights into maximising the performance and longevity of conveyor systems. Stay tuned as we explore the keys to proactive maintenance and operational excellence in the realm of conveyor system management.
Best Practices for Conveyor Belt Maintenance
In the bustling environment of industrial operations, the reliability and efficiency of conveyor systems are paramount to ensuring smooth production processes and optimal output. However, the continuous operation of conveyor belts in harsh environments inevitably leads to wear, tear, and potential breakdowns. Proactive maintenance practices are therefore essential to maximise the performance and longevity of conveyor systems, minimising costly downtime and ensuring uninterrupted production flow.
Regular Inspection and Monitoring: Implement a schedule for routine inspection and monitoring of conveyor belts, rollers, pulleys, and other components. Conduct visual inspections to identify signs of wear, damage, misalignment, or contamination. Utilise sensors and monitoring systems to detect anomalies in belt tension, speed, and alignment, allowing for early intervention before issues escalate.
Cleaning and Lubrication: Keep conveyor belts and components clean and free from debris, residues, and contaminants that may compromise performance or cause premature wear. Regularly clean belts, rollers, and pulleys using appropriate cleaning agents and methods. Apply lubricants as needed to reduce friction, prevent corrosion, and prolong the lifespan of moving parts.
Tension and Tracking Adjustment: Maintain proper tension and tracking of conveyor belts to ensure smooth and uniform movement along the conveyor system. Periodically check belt tension and adjust as necessary to prevent slippage or sagging. Monitor belt tracking to prevent misalignment, which can lead to uneven wear and premature failure of belts and components.
Replacement of Wear Parts: Keep a stock of spare parts on hand and replace worn or damaged components promptly to prevent unexpected breakdowns. Common wear parts include belts, rollers, bearings, and pulleys. Follow manufacturer recommendations for replacement intervals and ensure that replacements are installed correctly to maintain optimal performance and safety.
Training and Education: Provide comprehensive training to maintenance personnel on proper conveyor belt maintenance procedures, safety protocols, and troubleshooting techniques. Equip employees with the knowledge and skills necessary to identify and address maintenance issues effectively, minimising the risk of accidents, injuries, and downtime.
Documentation and Record-Keeping: Maintain detailed records of maintenance activities, including inspection reports, maintenance schedules, repair logs, and parts inventory. Track equipment performance over time to identify trends, anticipate maintenance needs, and optimise maintenance schedules for maximum efficiency and reliability.
By adhering to these best practices for conveyor belt maintenance, businesses can proactively manage the health and performance of their conveyor systems, reducing the risk of unexpected downtime, costly repairs, and production disruptions. In the final section of our exploration, we’ll gaze into the horizon of future trends and innovations in conveyor system management, offering insights into the evolving landscape of industrial automation and optimisation. Stay tuned as we embark on a journey into the future of conveyor technology and beyond.
Conclusion
As we conclude our journey through the realms of conveyor system management, one thing becomes abundantly clear: the future is bright with promise and potential. The evolution of conveyor technology—from simple mechanical systems to sophisticated, interconnected networks—reflects the relentless march of progress in the industrial landscape. By embracing emerging trends and innovations, businesses can unlock new levels of efficiency, productivity, and sustainability, positioning themselves for success in an increasingly competitive marketplace.
The integration of automation, artificial intelligence, and IoT connectivity heralds a new era of intelligent conveyor systems capable of adapting and optimising operations in real-time. Predictive maintenance technologies empower businesses to preemptively address maintenance issues, minimising downtime and maximising equipment lifespan. Modular and flexible designs offer unparalleled agility, enabling businesses to swiftly adapt to changing market demands and operational requirements.
Moreover, as industries embrace sustainability as a core value, conveyor system manufacturers are innovating with green and eco-friendly solutions that minimise environmental impact and promote resource efficiency. From energy-efficient motors to recyclable materials, these advancements reflect a commitment to stewardship and responsibility in the pursuit of industrial excellence.
As we stand on the cusp of this exciting future, let us not forget the essential role of human ingenuity and collaboration in driving innovation forward. It is through the collective efforts of visionary leaders, skilled engineers, and dedicated workers that the promise of tomorrow becomes a reality today. By fostering a culture of innovation, embracing technological advancements, and staying attuned to emerging trends, businesses can chart a course toward a future of unparalleled success and prosperity.
In closing, let us embark on this journey with optimism, determination, and a steadfast commitment to excellence. The future of conveyor system management holds boundless opportunities for those bold enough to seize them. Together, let us embrace the challenges and opportunities that lie ahead, forging a path toward a brighter, more sustainable future for industries and communities around the globe.
You’ve seen them in factories, sorting through mountains of metal. But have you ever stopped to think about the evolution of conveyor magnets? From their early developments to the latest advancements in dry-type magnet technology, there’s a fascinating history to uncover. Stick around as we delve into how they’ve transformed over the years and why they’re more important than you might think.
The Origin of Conveyor Magnets
You’ve probably wondered about the origin of conveyor magnets, haven’t you? It’s actually quite an interesting story that dates back to the early 19th century, during the height of the industrial revolution. Conveyor magnets were born out of necessity, as a solution to an industrial challenge that needed solving.
Factories were producing goods at an unprecedented scale, but they faced a problem. Metal debris was causing significant damage to machinery, and manual removal was time-consuming and inefficient. So, the innovative minds of the time developed the first conveyor magnets, a revolutionary invention that changed the face of industry.
The first conveyor magnets were relatively simple in design. They were essentially magnetic bars attached to a conveyor belt system. As the belt moved, the magnets would attract and hold onto any metal debris, preventing it from causing damage to the machinery.
Over time, these designs were refined and improved. Manufacturers started using stronger, more durable materials and implemented new magnetic technologies to increase efficiency and effectiveness. It wasn’t long before conveyor magnets became a staple in factories around the world.
Today, you’ll find conveyor magnets in a wide range of industries, from mining and construction to recycling and waste management. They’re an essential tool in maintaining a safe, efficient work environment, and their evolution is testament to the power of innovation and ingenuity.
Early Developments in Conveyor Magnets
After the initial creation of conveyor magnets in the early 19th century, you’ll find that their development didn’t stop there. Engineers and scientists alike began to understand the importance of these devices in the industrial sector, particularly for sorting and separating ferrous materials from non-ferrous ones in product lines.
The first major leap in development came with the introduction of electromagnets. Unlike their permanent counterparts, electromagnets could be turned on and off, giving you control over when and where magnetic force was applied. This innovation meant you could accurately sort materials with a level of precision that wasn’t possible before.
Despite this advancement, early conveyor magnets had their drawbacks. They were large, unwieldy, and consumed a significant amount of energy. The need for more efficient models was clear, and the industry responded. Engineers began to experiment with different shapes and sizes, leading to the development of the drum magnet. This design allowed for the magnet to rotate, offering continuous separation and improving overall efficiency.
The use of alloy materials, such as alnico and ferrite, also played a part in the early development of conveyor magnets. These materials offered higher magnetic forces and resistance to demagnetisation. In turn, these improvements led to magnets that were more effective, durable, and suitable for a wider range of applications.
As you can see, the early development of conveyor magnets was a time of experimentation and evolution, characterised by significant leaps in technology and design. These advancements laid the foundation for the sophisticated, high-performing conveyor magnets we use today.
Industrial Revolution’s Impact
The Industrial Revolution, with its focus on mass production and efficiency, dramatically changed how you’d use conveyor magnets. Before, they served simple, singular tasks, but with the advent of large-scale manufacturing, the demand for more complex applications surged. Conveyor magnets were no longer just a tool, they became an integral part of the production process.
With factories churning out products at an unprecedented rate, there was a need for a system that could handle the pace and volume. That’s where conveyor magnets came in. You’d find them in assembly lines, sporting goods, separating materials, and even in packaging processes. They made operations smoother, faster, and more efficient.
But it wasn’t just about quantity. The Industrial Revolution also emphasised quality. You’d want your products to be consistent, right? Conveyor magnets helped ensure that. By providing a reliable and precise method of material handling, they reduced the risk of errors and defects.
However, it wasn’t all smooth sailing. The early conveyor magnets had their flaws. They were prone to overheating and their magnetic fields weren’t as strong as you’d want them to be. But as with any technology, they evolved. Innovations were made, designs were improved. Today, you’ve got conveyor magnets that are durable, efficient, and incredibly powerful.
Technological Progress Post-1900s
Since the 1900s, there’s been remarkable technological progress that’s dramatically enhanced the capabilities and applications of conveyor magnets in your industry. With the advent of fully automated systems, conveyor magnets have become more efficient, reliable, and versatile. They’ve evolved from simple, manually-operated tools into sophisticated, computer-controlled machines capable of handling a wide range of materials and tasks.
In recent years, the development of dry-type magnet technology has been a game-changer. It’s allowed for the design of more compact, lightweight, and energy-efficient conveyor magnets. These magnets require less maintenance, have a longer lifespan, and offer superior performance compared to their older counterparts.
Advancements in material science have also played a critical role. The introduction of rare-earth materials, such as neodymium and samarium-cobalt, has resulted in magnets with greater magnetic force. These magnets can attract and hold heavier objects, expanding the range of materials that conveyor magnets can process.
Moreover, the integration of digital technology has revolutionised conveyor magnet operations. Modern systems come equipped with sensors, software, and wireless communication capabilities. These features enable real-time monitoring, remote control, and data analysis, enhancing efficiency and reducing downtime.
Conveyor Magnets in Modern Industries
In today’s fast-paced industrial landscape, you’ll find conveyor magnets playing an integral role, thanks to their enhanced capabilities and versatility. They’re used across various sectors, from mining to food processing, and you’d be hard-pressed to find a production line that doesn’t rely on them in some way.
Just consider the recycling industry. Conveyor magnets efficiently separate ferrous metals from other materials, significantly reducing manual labour and increasing the speed of the whole process. They’re the unsung heroes, tirelessly sorting through tons of waste, ensuring that everything that can be reused is, in fact, reused.
Or take the food processing industry. If you’re wondering how conveyor magnets fit in, think about the safety measures involved in food preparation. These magnets detect and extract any metallic contaminants that might have accidentally found their way into the food. They’re vital in maintaining the quality and safety of the food we eat.
In manufacturing, conveyor magnets lift, hold, and move heavy metal objects, improving efficiency and safety. They’re indispensable in automotive assembly lines, moving parts smoothly and swiftly without the risk of damage or injury.
And let’s not forget about the mining industry. Conveyor magnets are key in extracting valuable ferrous minerals and separating them from other substances.
With each passing year, advancements in dry-type magnet technology are making conveyor magnets even more capable and adaptable. They’re not just keeping pace with the demands of modern industries – they’re helping to shape them. As you can see, conveyor magnets truly are at the heart of our industrial world.
The Shift Towards Dry-Type Magnets
As you observe the transformative role of conveyor magnets in various industries, you’ll notice a significant shift towards the use of dry-type magnets. This change isn’t accidental; it’s driven by several key advantages that dry-type magnets offer over their traditional counterparts.
Firstly, you’ll find that dry-type magnets are easier to maintain. Unlike other types, they don’t require a cooling system, which eliminates the need for constant monitoring and maintenance. This means you’re looking at a significant reduction in operational costs, which, of course, is a huge plus for any business.
Secondly, dry-type magnets are more energy-efficient. In a world where sustainability has become a top priority, this feature can’t be overlooked. The absence of a cooling system means less energy is used, reducing the industry’s carbon footprint.
Lastly, these magnets offer improved performance. They’re designed to withstand high temperatures and harsh environments, making them more durable and reliable. As a result, they’re becoming the preferred choice in industries where conditions can be extreme, like mining and recycling.
But it’s not just about practical benefits. The shift towards dry-type magnets represents a broader trend in the industry: the move towards smarter, more sustainable solutions. It’s a reflection of how innovation is driving change, leading to improved efficiency and effectiveness in material handling processes.
Advancements in Dry-Type Magnet Technology
Now, let’s dive into the latest advancements that have come about in dry-type magnet technology, and how they’re changing the game for industries around the world. With the shift from wet to dry-type magnets, there’s been an explosion in innovation. Higher strength, more efficient, and more durable magnets are becoming the norm, providing a significant boost to productivity and efficiency.
One of the key developments is the rise of rare-earth magnets. These magnets are incredibly powerful and offer superior performance compared to traditional ferrite magnets. They’re perfect for high-intensity operations, where a strong magnetic field is required. Moreover, they’re also highly resistant to demagnetisation, ensuring they’ll last a long time even under harsh conditions.
Another breakthrough is the development of self-cleaning dry-type magnets. This advancement is a game-changer, as it drastically reduces the need for manual cleaning and maintenance. The magnet automatically disposes of the captured ferrous materials, saving you time and effort.
Lastly, we’ve seen a push towards more compact and lightweight magnets. This makes them more versatile and easier to integrate into existing conveyor systems. Despite their smaller size, these magnets don’t compromise on power or performance.
Benefits of Modern Conveyor Magnets
With the evolution of conveyor magnets, you’re not only getting a more powerful and efficient system, but also reaping a host of other benefits. Modern conveyor magnets offer increased durability and longevity, meaning you’re investing in a system that’ll last. They’re built with robust materials designed to withstand harsh conditions and heavy usage, so you’ll face fewer maintenance issues and lower replacement costs.
The second major benefit is improved safety. Conveyor magnets have evolved to include safety features that reduce the risk of accidents on the production line. They’re designed to automatically separate and remove ferrous materials, eliminating manual handling and reducing the risk of injury. This not only protects your employees but also helps avoid costly workplace incidents.
With modern conveyor magnets, you’re also getting a system that’s energy efficient. They’re designed to use less power, which not only saves you money on energy costs but also contributes to a more sustainable operation. In a world increasingly focused on environmental impact, this is a significant advantage.
The fourth benefit is enhanced productivity. Modern conveyor magnets are faster and more effective at separating and removing unwanted ferrous materials, which speeds up your production line and boosts your overall output. They’re also easy to use, reducing training time and making your operation more efficient.
Lastly, modern conveyor magnets are adaptable. They can be integrated into different conveyor systems and adjusted to handle various material types and sizes. This flexibility means you can tailor the system to your specific needs, which ultimately gives you more control over your operation. In short, the benefits of modern conveyor magnets are clear: they’re durable, safe, energy-efficient, productive, and adaptable.
Environmental Implications of Conveyor Magnets
In terms of environmental implications, you’ll find that the advancements in conveyor magnet technology are contributing significantly to sustainability efforts. This is largely because they’re designed to reduce energy consumption and minimise waste generation. You’ll appreciate how this technology is shaping our industrial practices towards a more eco-friendly future.
Now, you might be wondering how exactly conveyor magnets promote energy efficiency. Well, it’s mainly due to their ability to sort and separate materials without any physical contact. This means they don’t require as much energy to operate as traditional sorting methods, which typically involve more mechanical processes. Consequently, they’re reducing the overall energy footprint of industries that use them.
Then there’s waste reduction. You’ve likely seen how much waste is produced during manufacturing processes. With the use of conveyor magnets, industries can better separate and recycle materials, reducing the amount of waste that ends up in landfills. They’re even capable of extracting valuable metals from waste streams, which can then be reused. This circular approach to resource management is a key aspect of sustainable practices.
But it’s not just about the tangible benefits. Conveyor magnets also contribute to a cleaner, safer work environment by eliminating the need for manual sorting, which can expose workers to hazardous materials. So, while they’re protecting our planet, they’re also safeguarding the health of the workforce.
Future Prospects for Conveyor Magnets
Considering the substantial environmental benefits you’ve come to understand, it’s no surprise that the future for conveyor magnets is looking incredibly promising. You’ve seen how they’ve evolved over the years, becoming more efficient, reliable, and environmentally friendly. But what does the future hold for this transformative technology?
Firstly, it’s expected that conveyor magnets will become even more efficient. Advancements in dry-type magnet technology are paving the way for this. You’ll see machines that consume less energy, reducing operational costs and further lessening environmental impact. It’s a win-win situation for businesses and the planet.
Next, there’s the potential for increased automation. Conveyor magnets already play a crucial role in automated processes, but the future holds even more promise. Imagine a world where conveyor magnets can make real-time decisions based on the materials they’re handling, optimising processes on the fly.
Additionally, the demand for conveyor magnets is predicted to rise, especially in industries such as recycling, mining, and manufacturing. This growing demand will likely spur further advancements and innovations in the field.
Lastly, there’s the prospect of integrating conveyor magnets with other groundbreaking technologies. Think about a future where conveyor magnets are part of a larger, interconnected system, communicating with other machines and contributing to a fully integrated, smart factory.
Conclusion
So, you’ve seen how conveyor magnets have evolved over centuries, transforming industries and boosting efficiency. Today’s advancements in dry-type magnet technology bring not only productivity but also environmental benefits. It’s clear that the future of conveyor magnets is bright, with endless possibilities for further advancements. Keep your eyes peeled for what’s next, because this is one technological journey that’s not slowing down.